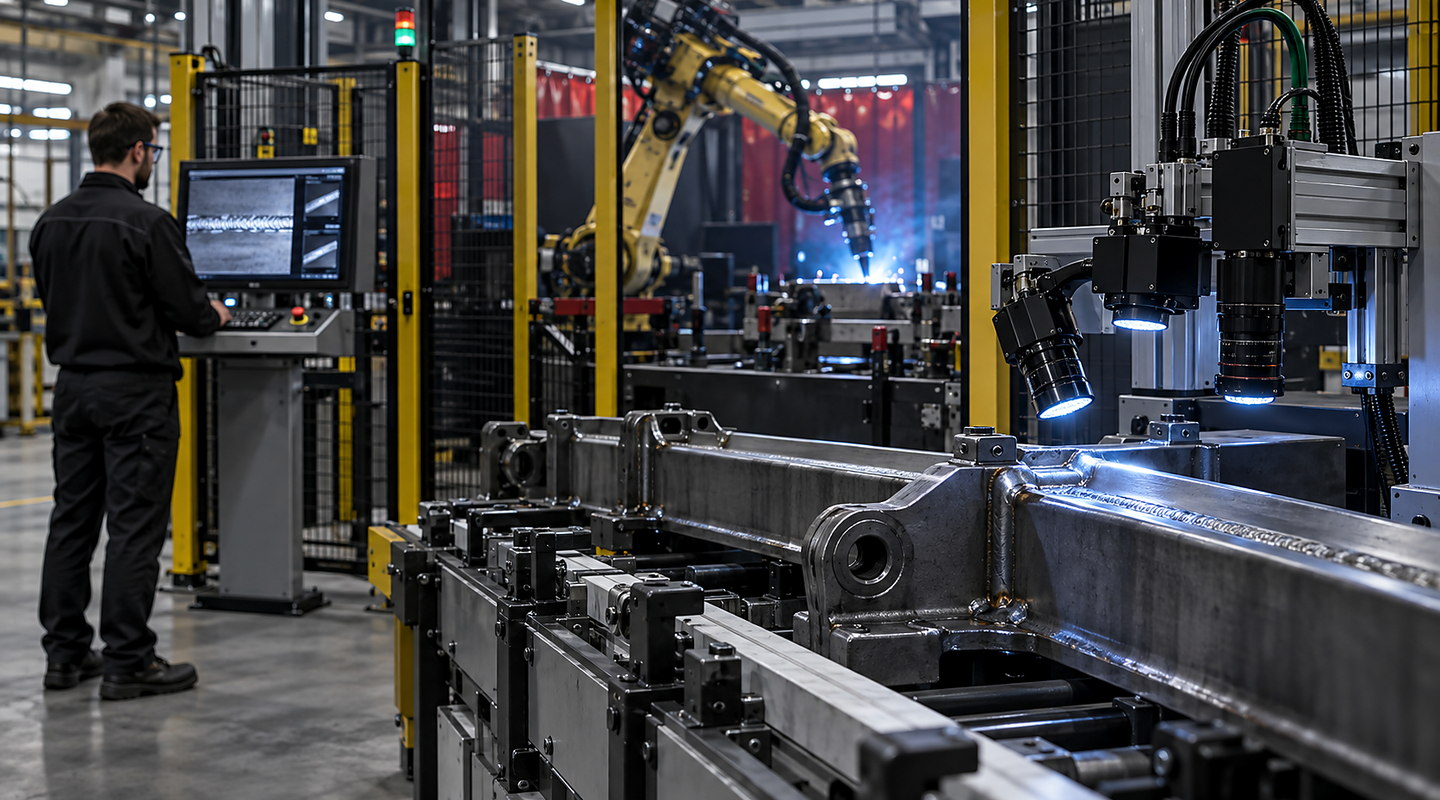
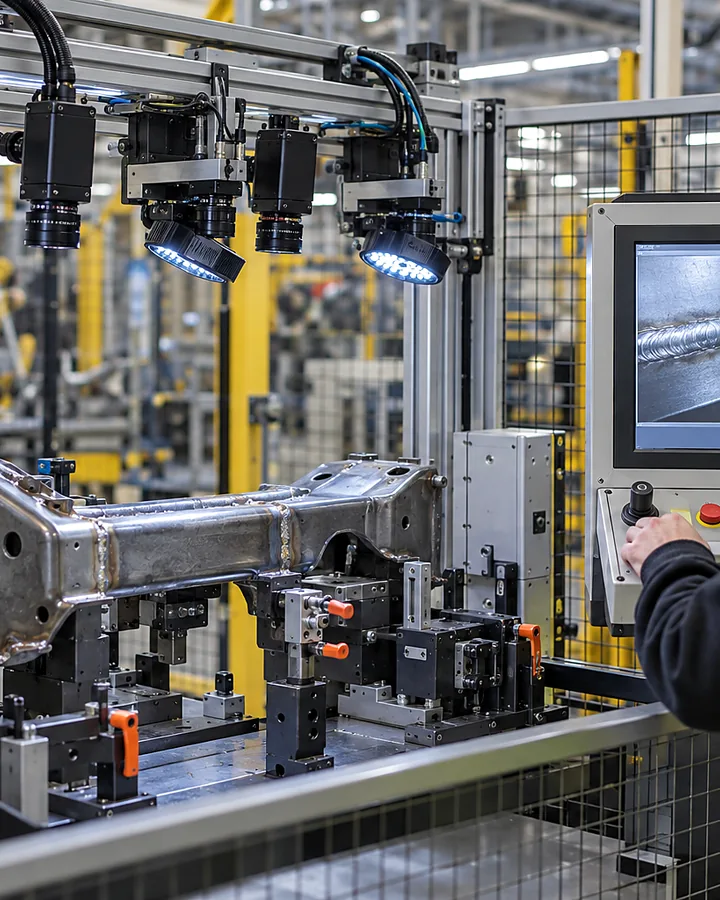
In-Line Inspection Using Visible Weld-Feature Inspection
Plan in-line inspection using visible weld-feature inspection around representative good, bad and marginal samples under real line presentation, line connections, operating limits, acceptance checks and next steps.
In brief
Define when the weld feature is presented, the time available to inspect it and the required response before the assembly moves on. Use representative good, bad and marginal samples at the intended operating pattern, following the optical trial and integration sequence before agreeing a layout.
Plan visible weld feature inspection around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems.
On the production floor
Plan for the conditions your team handles every day — Visible Weld Feature Inspection
Plan visible weld feature inspection around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. For in-line inspection using visible weld-feature inspection, the deciding details include visible defect or measurement definition for visible weld-feature inspection, part presentation and production speed and false-accept, false-reject and challenge criteria.
Details worth resolving early for in-line inspection using visible weld-feature inspection
Question 1
Visible Defect or Measurement Definition for Visible Weld-Feature Inspection
For in-line inspection using visible weld-feature inspection, describe the current position, required outcome, acceptable limits and known exceptions for visible defect or measurement definition for visible weld-feature inspection. That lets us compare options against your real production rather than one nominal value.
Question 2
Good, Bad and Marginal Sample Range
For in-line inspection using visible weld-feature inspection, describe the current position, required outcome, acceptable limits and known exceptions for good, bad and marginal sample range. That lets us compare options against your real production rather than one nominal value.
Question 3
Part Presentation and Production Speed
For in-line inspection using visible weld-feature inspection, describe the current position, required outcome, acceptable limits and known exceptions for part presentation and production speed. That lets us compare options against your real production rather than one nominal value.
Question 4
Optics, Lighting and Environmental Conditions
For in-line inspection using visible weld-feature inspection, describe the current position, required outcome, acceptable limits and known exceptions for optics, lighting and environmental conditions. That lets us compare options against your real production rather than one nominal value.
Question 5
Recipe, Reject and Line-Control Interfaces
For in-line inspection using visible weld-feature inspection, describe the current position, required outcome, acceptable limits and known exceptions for recipe, reject and line-control interfaces. That lets us compare options against your real production rather than one nominal value.
Question 6
False-Accept, False-Reject and Challenge Criteria
For in-line inspection using visible weld-feature inspection, describe the current position, required outcome, acceptable limits and known exceptions for false-accept, false-reject and challenge criteria. That lets us compare options against your real production rather than one nominal value.
Your operating cycle
Plan for more than automatic running
Include replenishment, normal production, planned change, short stops, fault recovery, cleaning and maintenance for in-line inspection using visible weld-feature inspection. A fast automatic step can still leave your team with a slow or awkward overall process.
Normal production and variant changes
Replenishment and material presentation
Operator access and safe interventions
Cleaning, maintenance and recovery
Prove the result
Test in-line inspection using visible weld-feature inspection against representative good, bad and marginal samples
Normal production
Run the agreed assembly mix and record the presentation and production speed for each trial condition. Compare observed decisions with the labelled samples across the planned repetitions, so the result remains tied to the conditions tested.
Difficult conditions
Include marginal good and bad examples and the credible extremes of the defined visible feature. Check the relevant variation in assembly presentation and optical conditions, recording which combinations were tested and which remain uncertain.
Fault and recovery
Agree what should happen when no valid inspection result is available. During the line trial, check the proposed fault indication, part handling and controlled restart against that plan; record anything not demonstrated.
Important limits
Be clear about what the trial has shown
A camera can only assess a property made visible and repeatable by the inspection setup.
Sample diversity and marginal cases determine how meaningful a feasibility result is.
Visual inspection does not replace hidden, destructive, functional or statutory tests.